Production Process
Ten key processes: the first three determine the material, the middle four the dimensions, and the last three whether it can leave the plant.
Ten key processes
Every process has work instructions, inspection items and an owner; key parameters are recorded for batch traceability.
Material forming
Incoming material inspection
IQCNylon pellets, rubber compounds, reinforcing yarn, metal fittings and seals are inspected batch by batch, checking material certificates and performance indicators; rejected batches are returned and recorded.
Formulation & batching
BatchingFormulation and batching follow product performance requirements, with batch numbers and ratios recorded so material batches stay traceable.
Tube extrusion
ExtrusionMulti-layer co-extrusion or rubber extrusion, with in-line monitoring of wall thickness, outer diameter and concentricity to keep the blank dimensionally stable.
Dimensional forming
Reinforcement & vulcanisation
Reinforce & CureAfter braided reinforcement, rubber hoses are vulcanised at high temperature with controlled temperature and time curves, ensuring cross-linking and pressure resistance.
End forming & over-moulding
End FormingOver-moulding, flaring and end forming ensure fitting bond strength and sealing-face accuracy.
Bending & cut-to-length
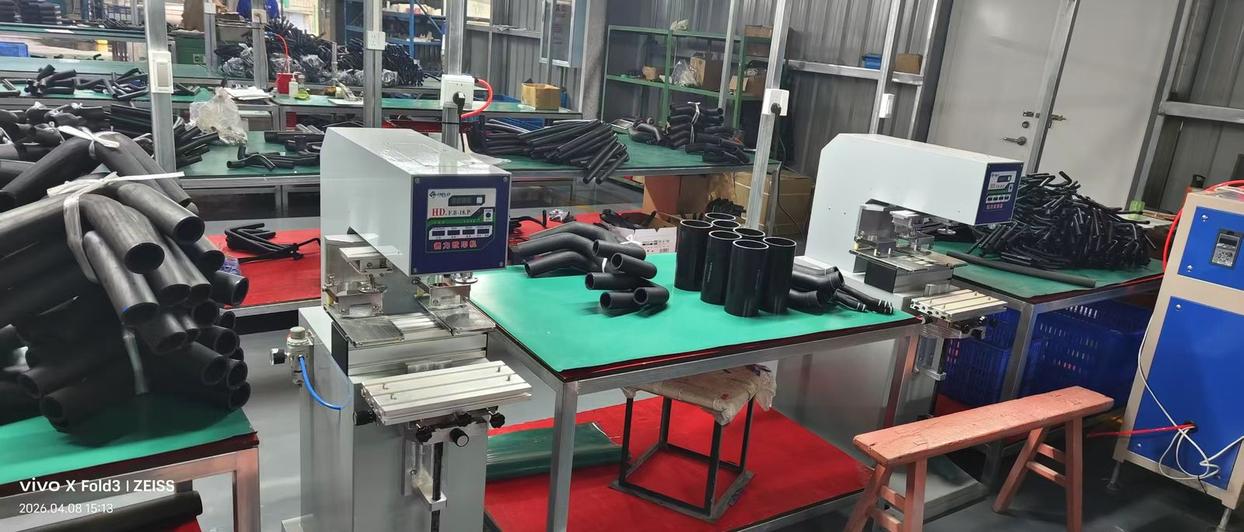
Bending & CuttingAutomatic bending and cut-to-length follow the 3D model; bend angle and length are checked against the drawing, and out-of-tolerance parts are segregated.
Assembly & crimping
AssemblyHoses, fittings, clips, brackets and quick-connect features are assembled and crimped, verified in line with dedicated gauges.
Testing & delivery
Performance testing
TestingBurst, tensile, airtightness and current tests are performed per the sampling plan, with records issued.
Final inspection & packing
OQCAppearance, markings, specification and packing quantities are checked item by item, with a certificate of conformity and batch traceability code attached.
Warehousing & delivery
DeliveryShipped in batches per order, supporting both domestic OEM supply and export customs packing requirements.
Three quality gates
From incoming materials to finished goods, specialists control every stage.
Incoming material inspection
Material certificates and key performance indicators are verified, samples kept per batch, and rejected batches isolated and returned — controlling quality risk at the source.
In-process patrol control
First-article and patrol checks cover wall thickness, outer diameter, bend angle and crimp dimensions; if out of tolerance, we stop and adjust immediately and trace parts already processed.
Final inspection before shipment
Airtightness, burst and other performance tests are sampled batch by batch; markings and packing quantities are checked, and goods are released with a certificate of conformity.
Process capability matrix
Key processes and inspection items for each product series are listed below, so customers can quickly judge whether a requirement falls within our capability.
| Single/multi-layer nylon tube assemblies | Co-extrusion · bending · quick-connect assembly · airtightness/burst |
|---|---|
| High-temperature fluorine brake hose assemblies | Extrusion · braided reinforcement · vulcanisation · crimping · burst/airtightness |
| Silicone hoses / air-conditioning lines | Extrusion · vulcanisation · cut-to-length · tensile/airtightness |
| Electrically heated urea lines | Assembly · circuit connection · current testing · airtightness testing |
| Resin hydraulic high-pressure steel-wire hoses | Spiral reinforcement · crimping · high-pressure burst · impulse durability |
| Fluoroplastic lines and assemblies | Extrusion · end forming · assembly · airtightness |
The table shows our standard process route; specific projects may add inspection items or adjust steps per the agreed technical protocol.
Need a hose solution or custom development?
Tell us your vehicle model, operating conditions and annual volume — we will reply with a selection and quotation proposal within one working day.